




Product Introduction
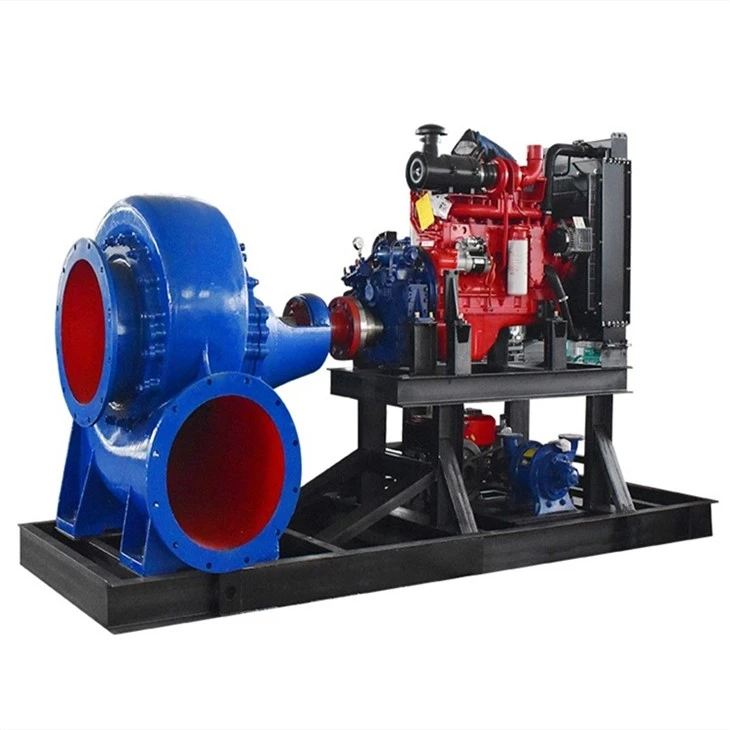
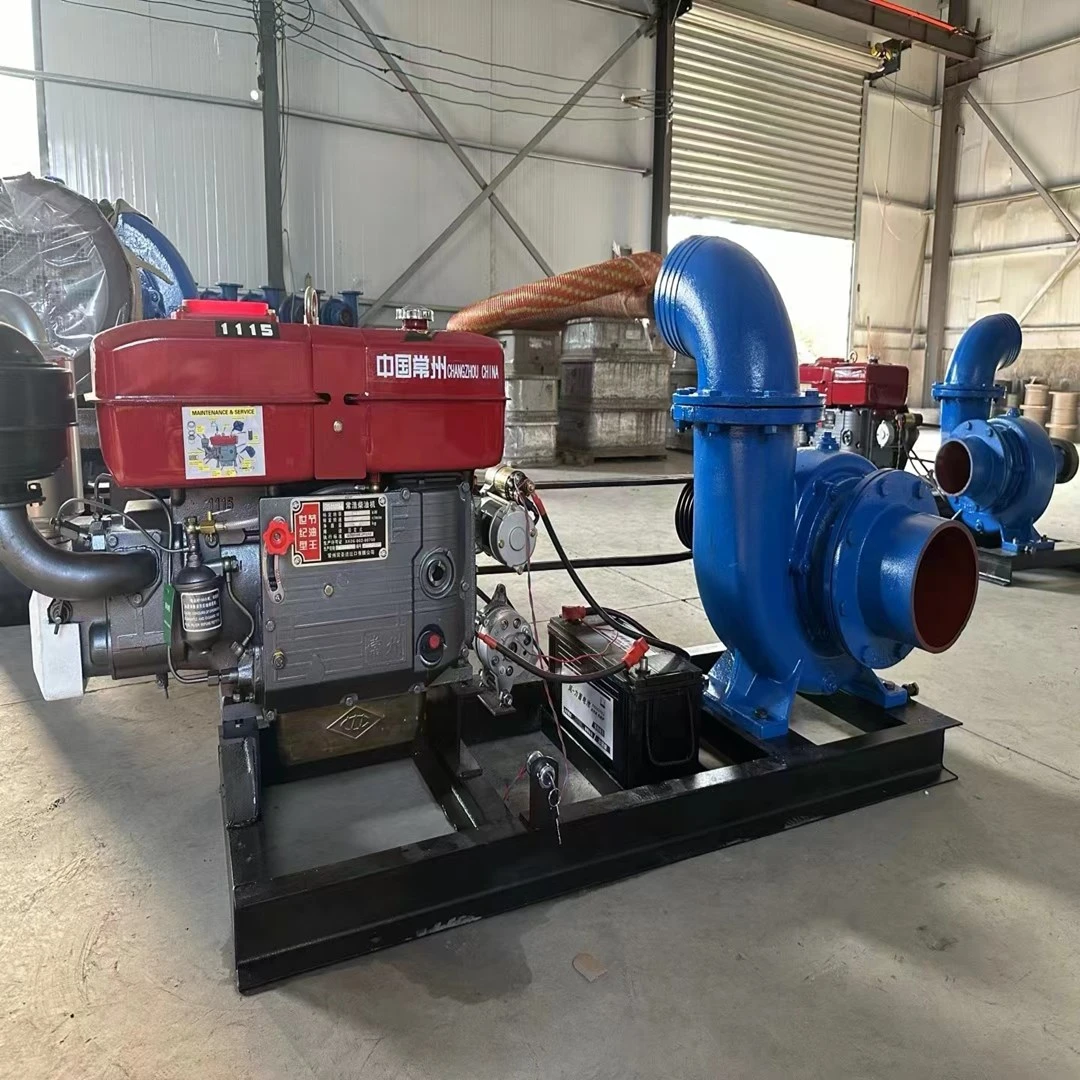
As an innovative equipment in the field of modern fluid transportation, the mixed flow pump truck combines the head advantage of centrifugal pumps with the flow characteristics of axial pumps, and adopts a direct coupled diesel engine drive system (optional Cummins/Weichai power) to achieve precise matching of 10-25m head in the flow range of 300-3000m ³/h. Its patented mixed flow impeller adopts the ternary flow theory design, which enables the fluid to obtain radial acceleration while advancing axially, saving 15% -20% energy compared to traditional pumps, and is particularly suitable for complex working conditions with large water level fluctuations. The equipment has passed CE and ISO9001 certification, with a protection level of IP68, and can operate stably in environments ranging from -20 ℃ to 50 ℃.
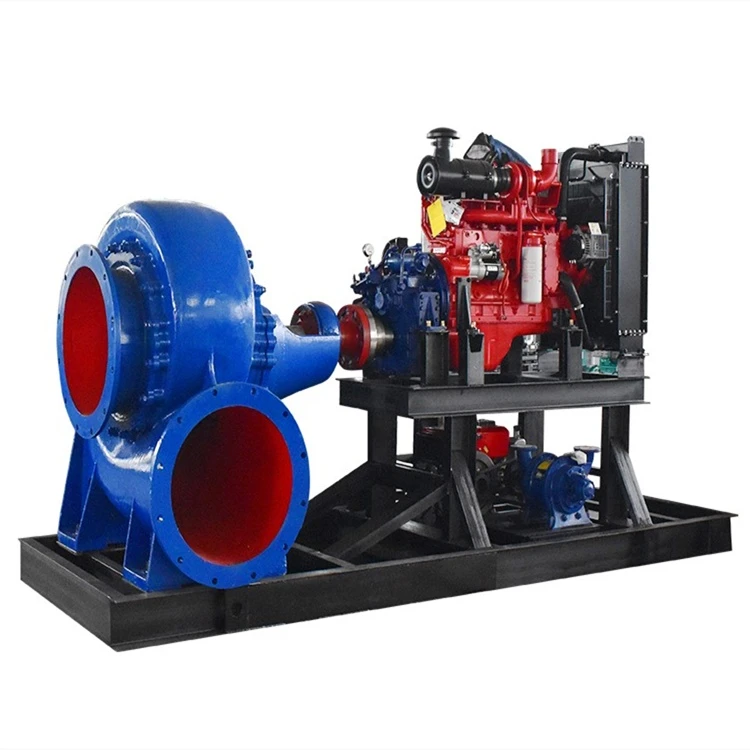
Product Features
1. Efficient Design
The impeller has been optimized through CFD fluid simulation, with 304 stainless steel integrated casting and mirror polishing process, achieving a peak efficiency of 87.5%. It can handle sewage media with sand content ≤ 15% and solid particles ≤ 20mm, and the hardness of the flow passage components is ≥ HRC55.
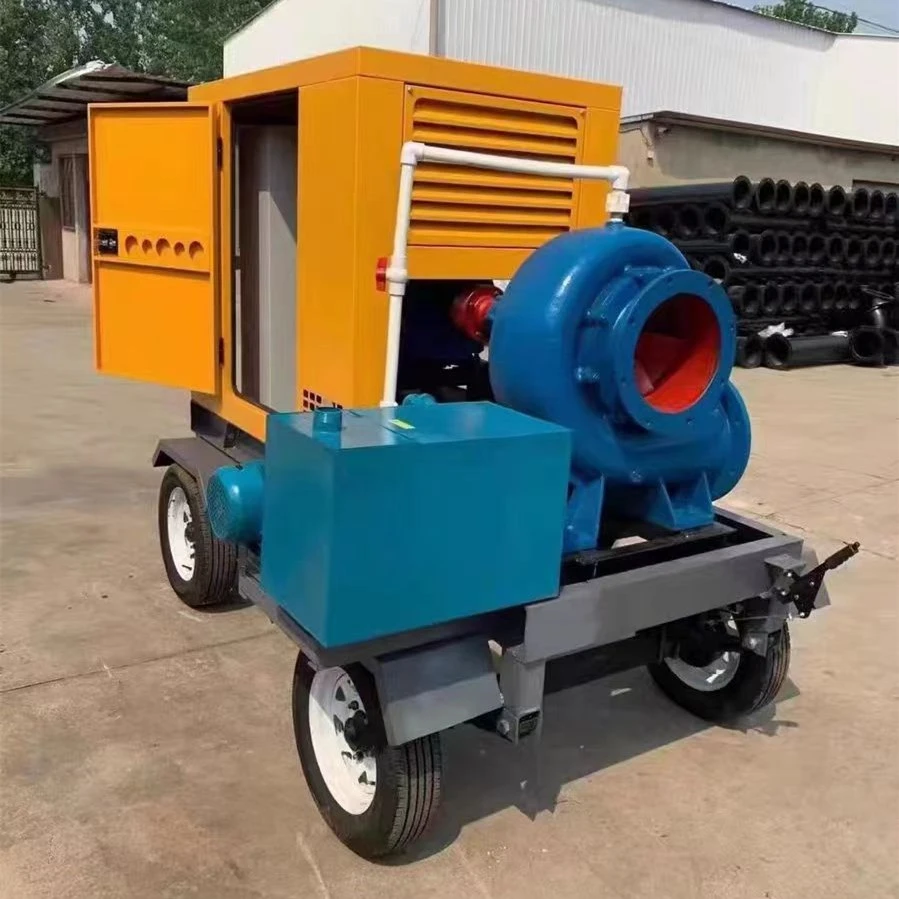
2. Mobile system
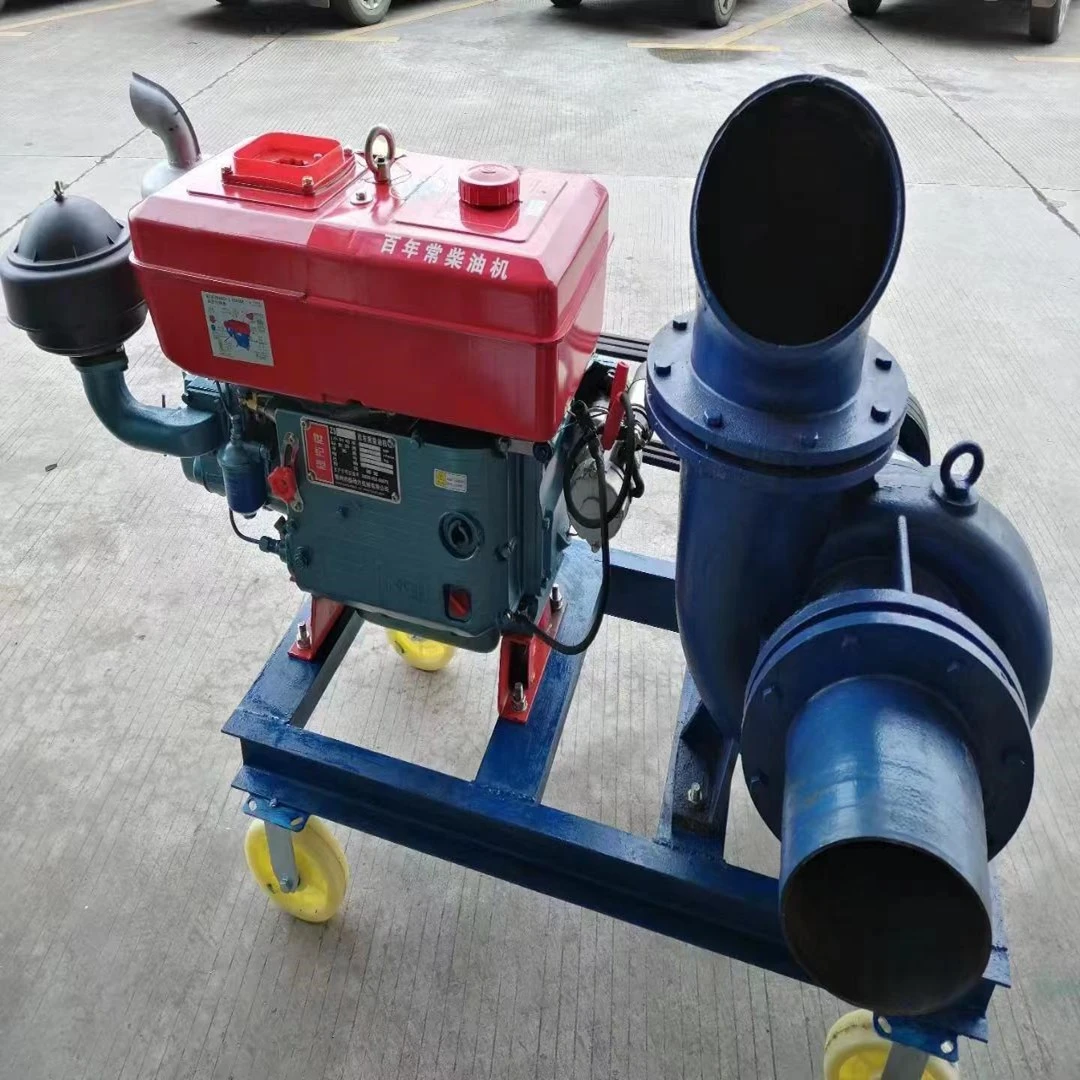
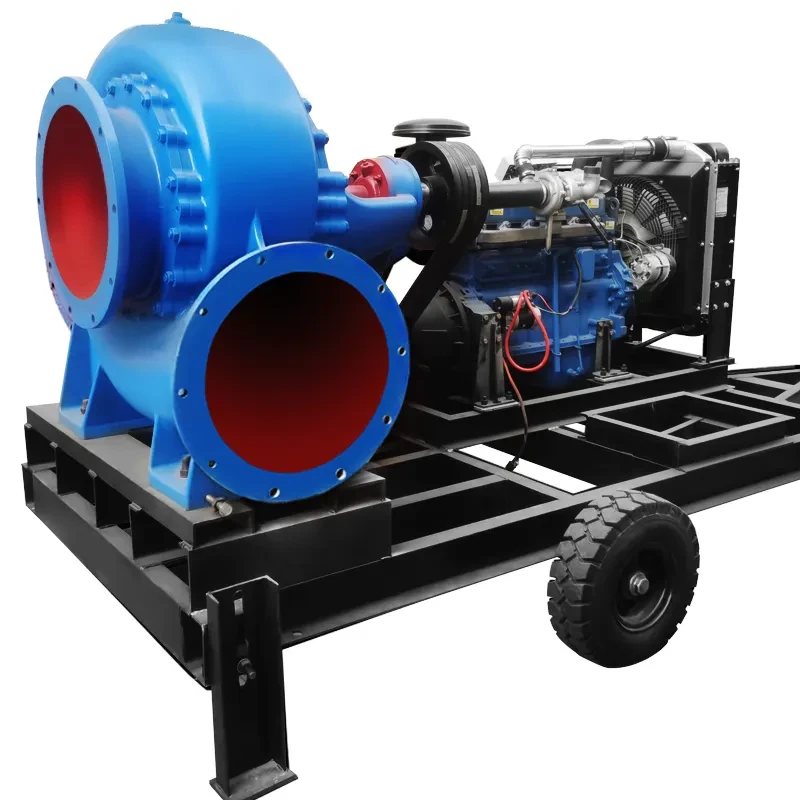
The modular trailer adopts a high-strength alloy steel frame, equipped with bidirectional hydraulic support legs (supporting force of 8 tons/piece) and 14 level explosion-proof tires. The tractor head is equipped with ABS braking system as standard, and the turning radius on rough roads is ≤ 6 meters..
3. Intelligent control system
Equipped with 4G/5G dual-mode IoT terminals, it can collect 12 parameters such as vibration, temperature, and speed in real time, automatically trigger sound and light alarms for abnormalities, and store historical data for up to 5 years. It supports seamless integration with smart water management platforms.
Key points of production
1. Material and process
The pump body is cast with resin sand and subjected to T6 heat treatment. The defect detected by X-ray inspection is ≤ Φ 1mm (GB/T 9444 Class 2), and the surface roughness Ra of the flow channel is ≤ 3.2 μ m.
2. Dynamic balance test
The impeller undergoes G6.3 dynamic balance verification at 2000rpm, with a residual unbalance of ≤ 1g • mm/kg. The matching shock-absorbing base ensures that the overall noise of the machine is ≤ 85dB (A).
3. Sealing system
The dual end mechanical seal adopts silicon carbide/graphite pairing, with an auxiliary flushing system pressure of 0.2-0.3MPa. The skeleton oil seal has a temperature resistance range of -40 ℃~120 ℃, which meets the API682 standard.
Advantage Analysis
|
Comparing dimensions |
Mixed flow pump truck |
Traditional centrifugal pump truck |
|
Comprehensive energy efficiency |
0.32kW • h/m ³ (adaptive adjustment for working conditions) |
0.45kW • h/m ³ (constant speed operation) |
|
Anti cavitation ability |
NPSHr ≤ 3.5m (with front induction wheel design) |
NPSHr≥5m |
|
System integration degree |
Integrated design including fuel tank and control cabinet |
External power distribution equipment is required |
Application scenarios
Urban flood control: With a continuous operation capacity of 7 × 24 hours, coupled with a sub mother pump set, it can form a graded drainage network. A single device can empty 1.5 meters of water from a standard football field (7140m ²) within 8 hours;
Precision agriculture: adapted to intelligent soil moisture monitoring systems, achieving a flow control accuracy of ± 5% through pressure compensation nozzles, meeting differentiated irrigation needs such as rice and orchards;
Mining management: The special stainless steel version can transport mine water with a pH value of 2-12, and the impeller anti winding design can pass through fiber impurities;
Industrial emergency: As a secondary emergency response unit for petrochemical enterprises, the explosion-proof model complies with the ATEX Directive 2014/34/EU standard and maintains a shaft seal leakage of ≤ 0.1mm under maximum head conditions.
Our factory
Hebei Jutong Pump Industry was founded in 2021 based on 35 years of pump technology accumulation, and quickly realized the full-chain production of slurry pumps, valves, and mechanical seals; in 2022, it passed the CAE simulation system and intelligent casting to obtain ISO/CE/MA triple certification, opening up the high-end market of mine environmental protection; domestic projects have accumulated 50,000+ hours of operation to verify equipment reliability, and 85% repurchase rate to build customer stickiness; in 2024, it will export Chilean copper mines and UAE desalination projects through multilingual digital platforms; in 2025, it will cover 50 countries along the "Belt and Road" and the goal of earning 50 million foreign exchange is imminent. If necessary, please contact us and we will provide you with professional advice.

Hot Tags: mixed flow pump truck, China mixed flow pump truck manufacturers, suppliers, factory, double suction pump truck


